Monday, 2 January 2012

ParCan MK2 HotEnd Developmant. Attempt 2 (Good Progress)

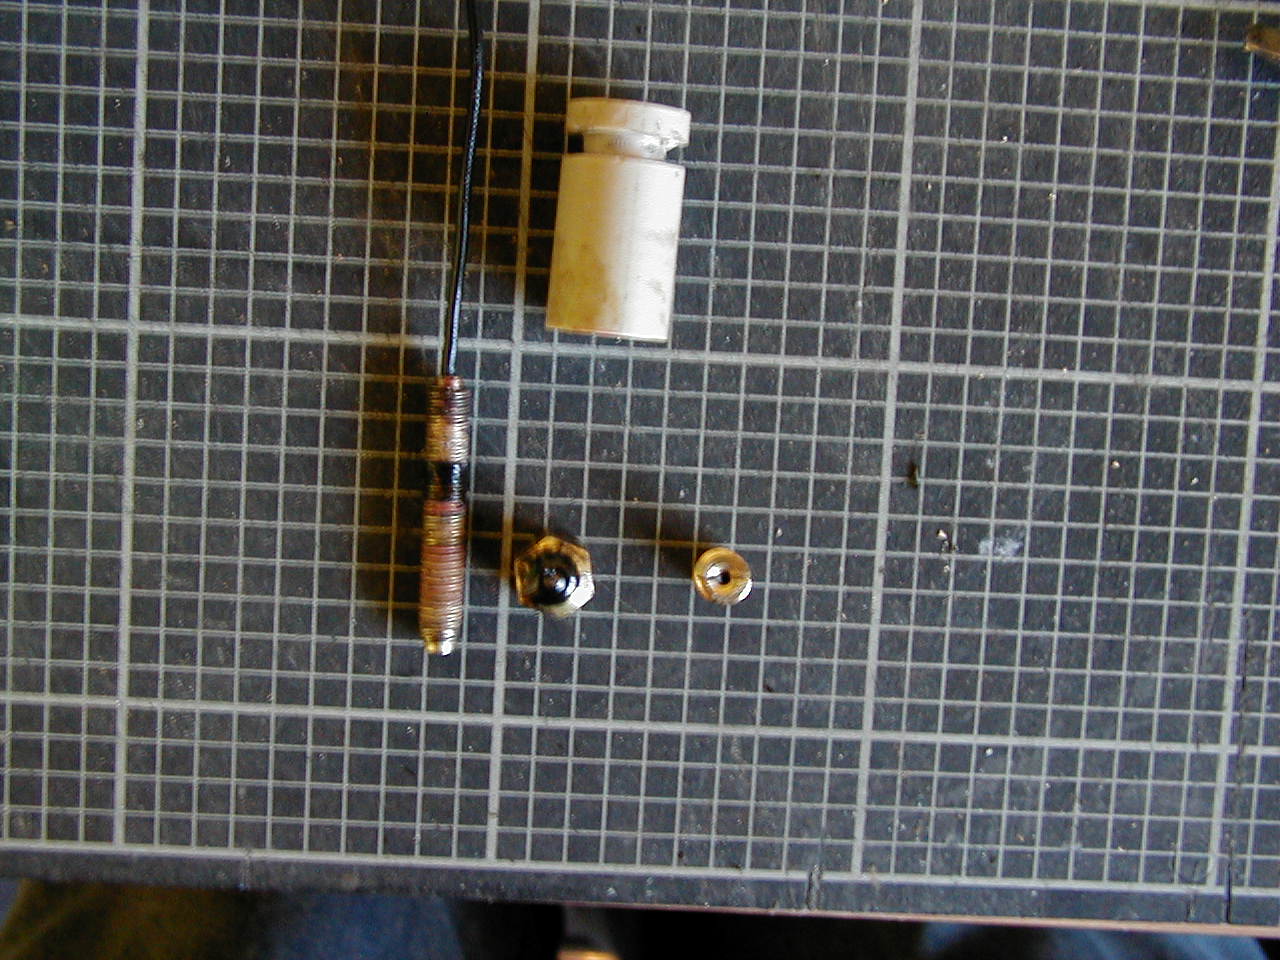
After the faults of the first attempt, this design attempts to create a Clamp for the PTFE tube.
I also dislike the idea of having the filament exposed to PEEK.
Using the lathe I drilled some M6 rod then turned down the end so that I could slide the PTFE tube over it.
As you screw the Brass / Tube into the PEEK, the idea is that the PEEK will clamp the PTFE tube.


I then made a new Brass Tube from M7 brass rod, drilled it 3.2mm for 3mm filament.
The PEEK is 15mm dia and 30mm long, drilled 15mm deep and tapped M7.
The rest of the hole is 5mm dia.


I then screwed up the nozzle so cut the tube down and screwed on one of my standard nozzles.

This is actually mounted on my Mendel at the moment amd prints reasonably well.
The tube interfce works but there is to much Thermal mass to get really nice prints.

I have created 2 more of this design with the nozzle as intended
These have been sent them out to some fellow reprappers to evaluate and do a write up.
If all is well, I will have these on sale in Mid januray.

ParCan MK2 HotEnd Developmant. Attempt 1 (FAIL)

After making well over 100 of my MK1 HotEnd kits, it's time to update the design.
Inspiration has been taken from my current design as well as the Makergear ideas.

For my first redesign I made a clone of the standard MG Hot end to see how well it worked.
This one was built for 1.75mm filament.
I will not be selling this design.
The PTFE Tube would ride up inside the PEEK causing the Filament to stick to the PEEK and jam.

After printing for about an hour, it had leaked down the Threads and also at the nozzle joint.

Disassembling the hot End reevealed that it just was not up to scratch, even after several modifications to try and make it work reliably.
I also have issues with trying to make this design work with 3mm filament.
Drilling 3.2mm down M6 threaded rod I can do, but there is very little metal left.
Later designs use M7 Threaded rods.
Parts List:
  1. 10mm Hex brass Nozzle. 0.5mm hole.
  2. M6 Threadeded Brass rod drilled 2mm for 1.75 mm filament.
  3. 15mm dia PEEK Rod, 30mm long. Drilled 15mm deep and tapped M6.
  4. The tube hole was drilled 3mm to accept 2mm ID PTFE tube.

The Top Of the PEEK was later drilled and tapped with a brass insert to stop the tube moving up.

Saturday, 19 November 2011

Mounting my Hot End

It's come to my attention that a few people have tried to use a Groove mount for my hot ends.

The White PTFE is not structural !

You MUST use the brown PEEK Block to mount and support my Hot End.
I have included a few mounting examples:

Using Wades geared extruder

This is the Wade Extruder from http://www.thingiverse.com/thing:11892 
Using Adrians extruder
And the mounting on my huxley.


Wednesday, 27 July 2011

Hybrid Huxley is coming along

I got Motors today. Zapp supplied them as they were in stock.


Note the very tidy work bench :)
 The Patented Belt clamps on the X axis
 You may be able to spot a few odd design issues.....


Sunday, 24 July 2011

Thermistor table for my thermistors.

Several people have asked me for this so here goes.


// /usr/local/bin/createTemperatureLookup.py --r0=100000 --t0=25 --r1=0 --r2=4700 --beta=4267 --max-adc=1023
// r0: 100000
// t0: 25
// r1: 0
// r2: 4700
// beta: 4267
// max adc: 1023
#define NUMTEMPS 20
short temptable[NUMTEMPS][2] = {
   {1, 713},
   {54, 236},
   {107, 195},
   {160, 172},
   {213, 157},
   {266, 144},
   {319, 134},
   {372, 125},
   {425, 117},
   {478, 110},
   {531, 103},
   {584, 96},
   {637, 89},
   {690, 83},
   {743, 75},
   {796, 68},
   {849, 59},
   {902, 48},
   {955, 34},
   {1008, 3}
};

Wednesday, 20 July 2011

My Hot-End design and other details.

It's about time I updated and wrote about this.

In the past I write about various Hot-End failures, so I designed my own hot end which still works and I still use from time to time.
That Hot end works well but is VERY Dribbly, resulting in rather untidy prints.

I put together an updated standard Reprap hot-end :
http://www.reprap.org/wiki/Geared_extruder_nozzle
This also failed. The PTFE split where it screws into the Brass Nozzle.

Several design ideas later I found a combination that prints cleanly and is strong enough.


The Nozzle is unchanged from the standard reprap design.


The PTFE has a shoulder turned onto it at 10.5mm dia X 4 mm long.


The PEEK is drilled to 8mm then 10.5mm approx 6mm deep.


The PTFE sits inside the PEEK block supporting it.


 The Heater I make 8 mm thick, rather than 10mm. It's Pictured here with resistor and Thermistor installed.

This has proven a strong and resillient Hot-End.
I have made and sold a good few of these with no complaints.
You will find these hot ends on sale at http://www.emakershop.com